
Scaling a beauty brand from direct-to-consumer (DTC) traction to wholesale distribution exposes structural vulnerabilities in supply chain planning. While formula development often captures the spotlight, packaging procurement represents the true operational bottleneck. Premium personal care and fragrance categories rely disproportionately on glass containers to communicate efficacy and brand prestige.
Yet, emerging brands frequently stumble when transitioning from generic stock containers to custom glass tooling. Multi-cavity molds, unpredictable production lead times, and prohibitive minimum order quantities (MOQs) tie up critical operating capital. Mitigating these risks requires operational rigor across tooling economics, dimensional tolerance control, and total cost of ownership (TCO) modeling.
The Scaling Paradox: Why Custom Glass Tooling Stalls Emerging Beauty Brands
Stock Components vs. Custom Mold Economics
Emerging brands routinely begin by sourcing off-the-shelf stock glass bottles from regional distributors. While this minimizes upfront development expenditure, it introduces severe strategic liabilities as operational volume expands:
- The Shelf Homogeneity Trap: Off-the-shelf silhouettes leave brands vulnerable to visual imitation, eroding premium pricing power on crowded retail shelves.
- Component Incompatibility: Generic glass threads often fail to match third-party custom pumps perfectly, triggering micro-leaks or skewed closure alignments.
- The Legacy Mold Capital Barrier: Traditional automated glass plants operate massive regenerative furnaces requiring minimum batch runs of 50,000 to 100,000 units, creating unsustainable capital lock-up for growing labels.
Shortening the Prototyping Cycle from CAD to Pilot Samples
In the fast-moving beauty sector, missing a seasonal holiday launch or retail onboarding window compromises market momentum. Legacy mold fabrication cycles typically consume four to six months before initial commercial units arrive.
For emerging cosmetic and fragrance houses, the traditional manufacturing barrier has always been capital-intensive minimum order quantities. To mitigate this inventory risk, modern procurement workflows prioritize manufacturers offering flexible production matrices. Operational benchmarks from custom glass bottle manufacturer Hua Glass demonstrate that combining rapid 14-day design prototyping with low 1,000-piece starting volumes enables indie beauty labels to test market-responsive custom silhouettes without absorbing prohibitive tooling overhead.
Compressed development cycles allow operators to validate market demand systematically:
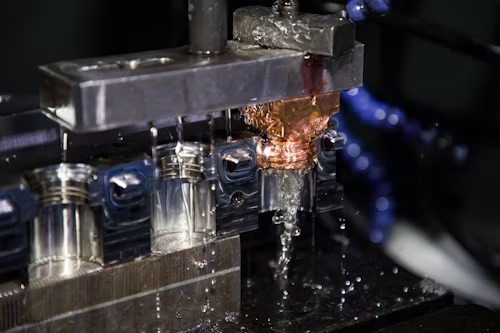
- Digital 3D CAD Simulations: Precise finite element modeling identifies glass wall-thickness stress points prior to cutting steel.
- Rapid Pilot Sampling (10–14 Days): Precision CNC trial molds deliver physical samples for volume validation and formula compatibility testing.
- Commercial Steel Tooling (30–40 Days): High-grade alloy mold sets transition from trial validation directly into high-efficiency pilot manufacturing runs.
Structural Integrity and Tolerance Control in Liquid Packaging
Critical Sealing Interfaces: Crimp vs. Screw Neck Finishes
The geometric junction where the container neck meets the closure assembly represents the most failure-prone interface in liquid personal care packaging:
- Crimp-On Finishes (FEA 15/20): Standard for fine fragrance, crimped collars compress an elastomeric gasket under an aluminum skirt, creating a permanent, tamper-proof seal impervious to atmospheric pressure changes.
- Screw Neck Finishes (GPI/DIN Standards): Essential for refillable beauty and treatment oils, threaded necks require strict thread pitch consistency. Variations exceeding 0.25mm cause thread stripping or cap tilting.
- Capillary Leak Pathways: Inadequate glass rim planar flatness creates micro-channels where low-viscosity alcohol or volatile botanical oils migrate via capillary action.
Four-Stage Quality Inspection Protocols
Maintaining high bottling yields across automatic filling lines demands rigid quality gates at the glass manufacturing facility:
- Rim Planar Flatness Verification: Laser profile scanners check the bottle mouth to verify zero warping, ensuring a true hermetic closure under torque.
- Wall-Thickness Uniformity: High-frequency sonic gauges measure glass distribution, confirming sidewalls maintain adequate density and impact resistance.
- Polariscopic Annealing Analysis: Optical polariscopes evaluate residual internal stresses, preventing sudden thermal shock fractures during hot-fill processes.
- Vacuum Chamber Leak Testing: Packaged units are submerged under negative pressure (-0.06 MPa) to guarantee closure hermeticity under transport stress.
Component Harmonization: Calibrating Pumps, Actuators, and Closures
Hydraulic Resistance and Delay-Mist Performance
Pairing high-end glass bottles with mismatched pump hardware degrades the customer touchpoint. Fluid dynamics dictate how different formulations discharge through internal actuator chambers:
- Formulation Viscosity Matching: Low-viscosity perfumes require tighter internal orifices to create fine aerosol clouds, whereas lipid-rich serums need wider intake valves to prevent hydraulic resistance.
- Delay-Mist Pre-Compression: Calibrated internal springs build internal pressure prior to valve release, delivering a prolonged, luxurious spray plume rather than an aggressive jet.
- Output Metering (1.0ml vs. 1.3ml): Precision dosing controls liquid consumption per pump, directly aligning product experience with customer usage guidelines.
Preventing Air-Pocket Ingress During High-Altitude Transit
Global supply chains subject packaged cosmetics to dynamic air pressure drops during air cargo transit and high-elevation land shipping:
- The Pressure Differential Factor: Cabin pressure decreases can create a suction delta that pulls liquid past standard closures if gasket durometers are uncalibrated.
- Dip-Tube Flexion: Engineered dip-tubes must feature angled base cuts and dimensional memory to maintain fluid intake without curling or suctioning against the bottom glass plate.
Key Takeaways
| Area | Key Takeaway | Impact/Data |
| Tooling MOQ | Bypass legacy furnace volume barriers | Slashes minimum run from 100k to 1,000 units |
| Prototyping | Deploy rapid CNC pilot tooling | Cuts sampling lead time to 10–14 days (vs. 4–6 mos) |
| Tolerance | Enforce strict screw-thread calibration | Discrepancies >0.25 mm strip threads and leak |
| QA Protocol | Mandate negative-pressure immersion testing | Guarantees hermetic seals under -0.06 MPa |
| Logistics TCO | Require cell dividers and safety inventory | Keeps breakage <0.5%; buffers 60-day delays |
Total Cost of Ownership (TCO) in Overseas Glass Sourcing
Balancing Unit Price Against Breakage Allowances and Buffer Stock
Evaluating offshore glass suppliers purely on ex-factory unit pricing leads to severe landed cost miscalculations. Strategic sourcing operations assess full landed expenditures:
- Transit Breakage Provisions: High-grade export packaging utilizes double-wall corrugated cartons and cell-partition dividers to hold transit breakage rates below 0.5%.
- Predictive Inventory Buffers: Maintaining a 60-day safety stock cushion protects brand cash flow against ocean freight disruptions and seasonal port bottlenecks.
Mitigating international logistics volatility requires brand operators to move past simple per-unit manufacturing costs toward total landed cost calculations. Strategic supply chain analysis published by Forbes reveals that operational transparency, standardized transit palletization, and predictive inventory buffers significantly outperform pure low-cost bidding, ensuring product release dates remain protected against maritime distribution friction.
By integrating agile, low-MOQ tooling workflows with rigorous quality inspection protocols, expanding beauty brands preserve liquidity, secure custom shelf differentiation, and safeguard their bottom-line profitability.
